8 min read
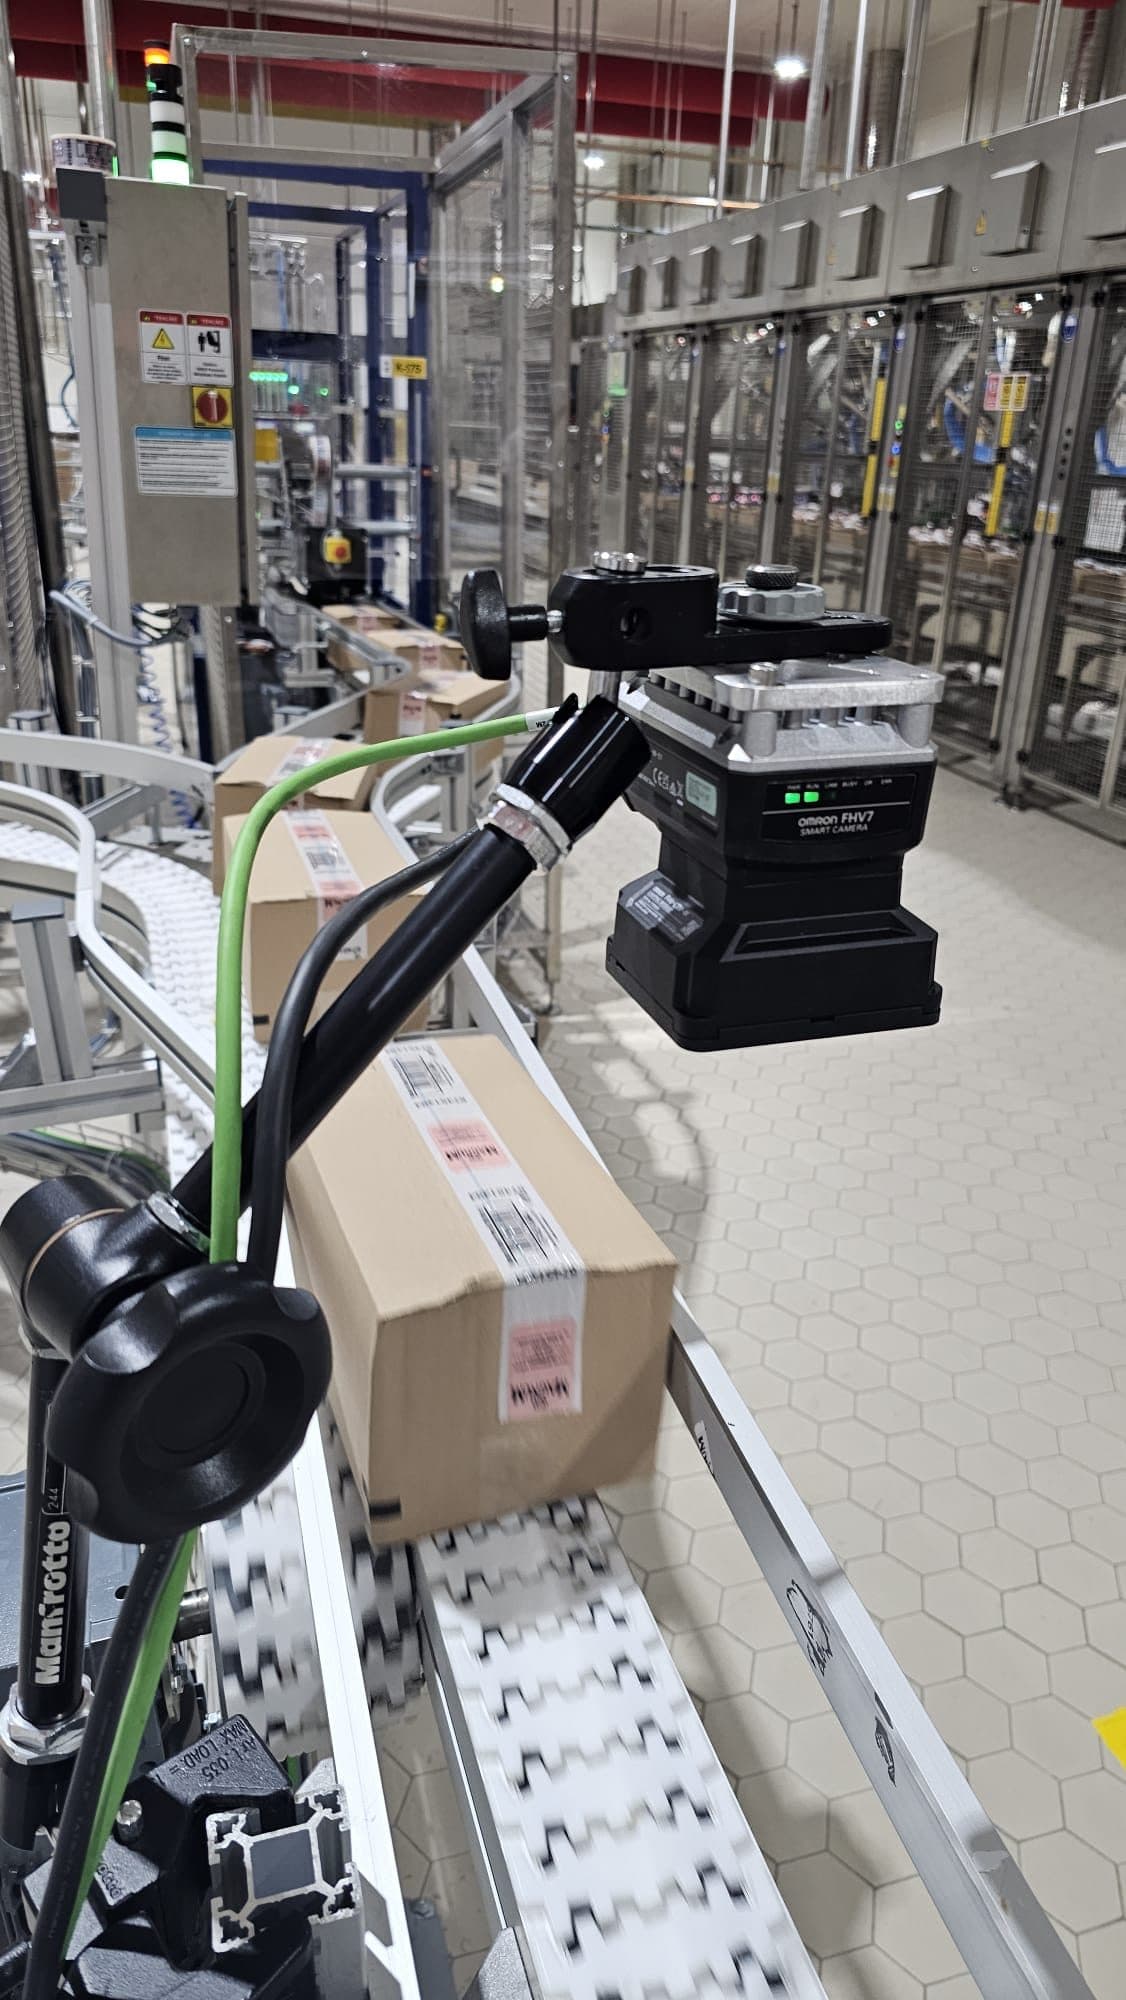
Starting a vision project by choosing the camera is like starting a panel project by choosing the cable. The first question is whether the defect separates from sound material in the image. If it does not, the most expensive camera in the world will not see it. What creates that separation is the light.
Five lighting techniques and where they are used
| Technique | Where the light comes from | Good for | Poor for |
|---|---|---|---|
| Direct | From beside the camera | Print, labels, colour | Surface scratches, glossy surfaces |
| Grazing | At a very shallow angle to the surface | Scratches, dents, embossing | Reading flat print |
| Backlight | From behind the product | Dimensions, holes, edges, seals | Surface defects |
| Dome | Diffuse, from all directions | Glossy and curved surfaces | Sense of depth |
| Coaxial | Along the camera axis via a mirror | Flat glossy surfaces, marks on metal | Deep surfaces |
The same defect, two different outcomes
Picture a shallow scratch on a matt, light-coloured surface. Under direct light the brightness difference between the scratch and sound material is almost zero, and it disappears in the image. Send the light in at a grazing angle and the scratch casts a shadow, making the contrast clear. The camera, lens and algorithm have not changed — only the angle of the light.
Glossy surfaces: the hardest case
On metal tins, coated packaging or glossy plastic, light reflects as it would off a mirror. That reflection causes trouble in both directions: it can mask a real defect, or look like one that is not there and produce a false reject. The answer is dome lighting — because the light arrives diffusely from every direction, no single hotspot forms.
Ambient light: the project's silent enemy
Factory lighting changes through the day, daylight comes in through windows, and lamps go on and off at shift change. In a system doing colour inspection, that variability feeds straight into the measurement: the same product reads differently in the morning and the evening. For colour and sensitive surface inspection, the camera area is therefore enclosed and only its own lighting is used.
Line speed, exposure and blur
The image is captured as the product passes the camera. If exposure is long, the product travels during that time and the image blurs; on a blurred image neither OCR reads nor measurements come out right. Shortening exposure demands more light. So as line speed rises, so must lighting power — the two are linked and are calculated together at setup.
Rule-based or AI?
Once the lighting is right, the method is chosen. For dimensional checks, presence/absence, barcodes and OCR, a rule-based method is faster, more predictable and cheaper. Where a defect's shape differs every time — creasing, crushing, an irregular stain — showing examples beats writing rules, so an AI model is preferred. In most projects the two work together.
Describe the defect you need to catch on your line, or send a photo of the product; we will assess feasibility with trial images and draw up the hardware list together.
Frequently asked questions
Can a vision system be retrofitted to an existing line?
Yes, most applications are retrofitted. Three things are needed: enough mounting space for camera and lighting, a trigger signal telling the system the product is passing, and a mechanism to remove the faulty product. Where there is no rejector, the product can be marked first and removed at a later station.
Colour camera or greyscale?
If the defect is not about colour, greyscale is better: processing is faster, resolution is used more efficiently, and no recipe update is needed when the material colour changes. A colour camera is only required where the decision genuinely depends on colour — packaging colour checks, wire colour sequence, label verification.
What happens if the system rejects a good product?
Every rejected product's image is recorded. The quality team reviews them to see why a false reject occurred; the threshold is adjusted or the image is added to training as an OK sample. In a setup that keeps no records this correction is impossible, the system loses trust over time and operators switch it off.
We have many product variants — does each need its own setup?
No. Each product type is stored as its own recipe holding the window position, tolerance and acceptance threshold. The operator selects the recipe on screen at changeover. Only when a product with very different geometry or surface character is introduced may the lighting angle need reviewing.
How is the return on investment calculated?
On two items: the cost of a defective product reaching the customer (recall, re-sorting, returns, reputation) and the cost of work wasted on the line. When a faulty product enters later stations, the labour and material spent on it are also lost. On most lines the sum of the two covers the investment quickly.