8 min read
The most common mistake in PLC selection is buying exactly what today's list requires. A few extra signals always appear during commissioning: a forgotten limit switch, an indicator lamp asked for late, a temperature sensor added while setting up. A project sized exactly to its I/O list ends up adding a module on site.
Start with the signal list
| Signal type | Typical source | What to watch |
|---|---|---|
| Digital input (DI) | Buttons, limit switches, sensors, relay contacts | 24 V DC or 220 V AC; sourcing/sinking (PNP/NPN) |
| Digital output (DO) | Relays, contactor coils, indicator lamps | Relay or transistor output; switching current |
| Analogue input (AI) | Temperature, pressure, level, flow | 4–20 mA or 0–10 V; resolution (bits) |
| Analogue output (AO) | Drive speed reference, valve position | Load impedance; isolation |
| Special | Encoders, high-speed counters, PT100 | Standard modules are not enough; a dedicated card is needed |
The protocol choice cannot be changed later
Which devices the PLC will talk to has to be clear from the start. Drives, power meters, smart cameras, weighers, barcode readers — each may speak a different protocol. Modbus RTU is the most widespread and cheapest but it is slow. Profinet and EtherCAT are fast and essential where motion control is involved. Changing protocol usually means changing the PLC.
HMI: what is shown matters more than screen size
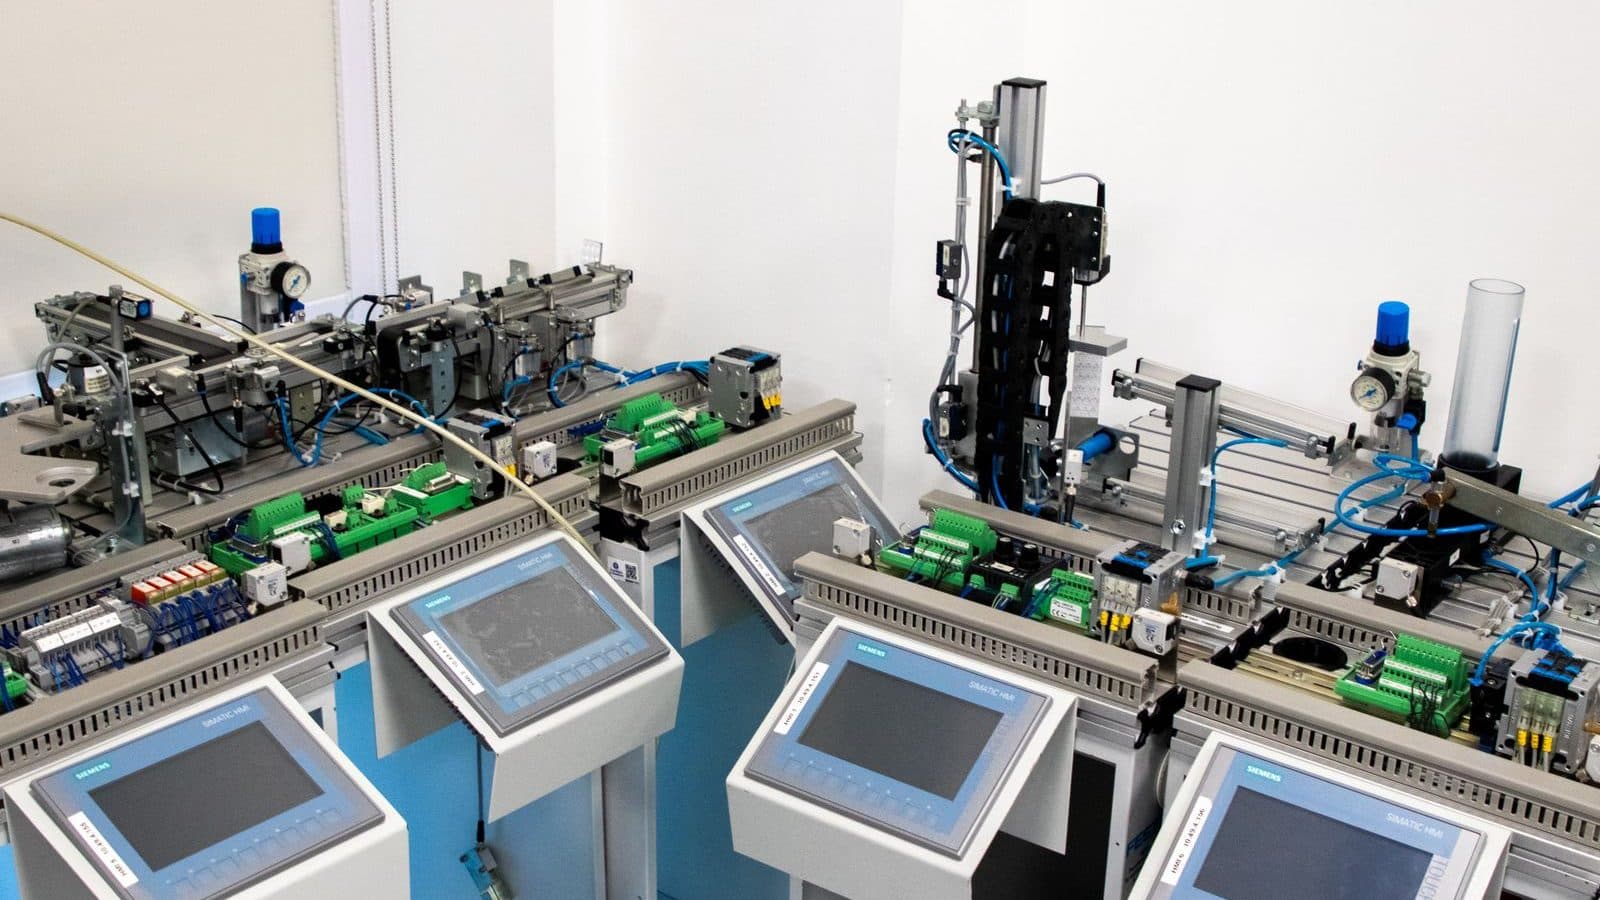
Operator panel size is usually chosen on looks. The right method is to sketch the screen pages first: how many values will be read, how many buttons there will be, whether there is an alarm list and a recipe page, whether trends are wanted. Seven inches is enough for most machines; control-room screens watching a whole line need 15 inches and up.
- Alarm list and history — the fastest route to a fault; hard to add later.
- Recipe management — essential where there are product variants; keeps operators out of parameters.
- User levels — so not everyone reaches the parameter screen.
- Trend graphs — make problems visible on variables such as temperature and pressure.
The value of staying in one family
If the plant already runs a PLC family, staying with it on a new machine brings three concrete benefits: spares are shared, the maintenance team learns no new software, and a module can be borrowed from another machine during a breakdown. The price difference is usually smaller than those three combined.
Send your signal list or describe what the machine will do; we will draw up the PLC, HMI, module and communication list together. Working with Omron, Siemens, Inovance and Schneider Electric, we can offer several budget levels for the same requirement.
Frequently asked questions
Should I choose a relay-output or transistor-output PLC?
A relay output switches both AC and DC and carries more current, which suits contactor coils and lamps. Its mechanical life is limited and it cannot switch fast. A transistor output is DC only and lower current but very fast, which is essential for servo and stepper pulse signals or fast valve control. Most panels use both.
Does the PNP/NPN sensor difference affect PLC selection?
Yes. The PLC's digital input card works as either sourcing or sinking and must match the sensor type. PNP sensors with sinking inputs are common in Europe, NPN in the Far East. Mixing them means the signal simply never appears. Confirm which type the plant uses before commissioning.
Who should hold the PLC program backup?
At the plant. If the program stays only with the contractor, the system is locked the day a change is needed years later or the contractor changes. On the projects we run, the program backup goes into the handover file with its comments and in an openable format.
Is a smart relay enough instead of a PLC for a small machine?
Where signal counts are low and the logic simple, a logic relay is both cheaper and sufficient. Draw the line here: if analogue processing, communication, recipes or alarm history are needed, move to a PLC. And if the machine may be extended later, buying a PLC now costs less than replacing everything in six months.